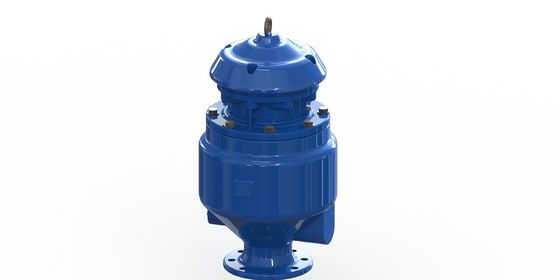
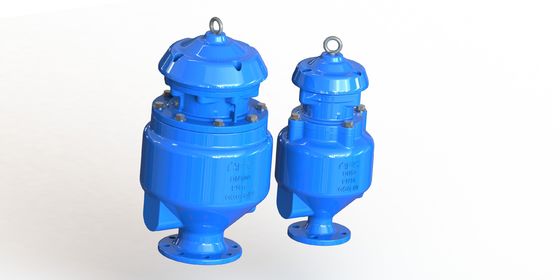
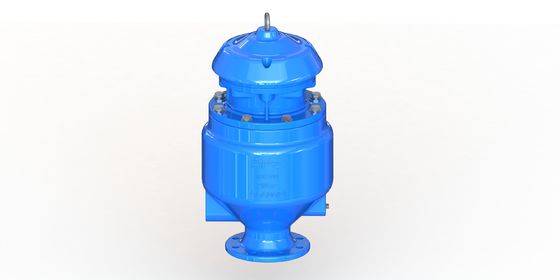
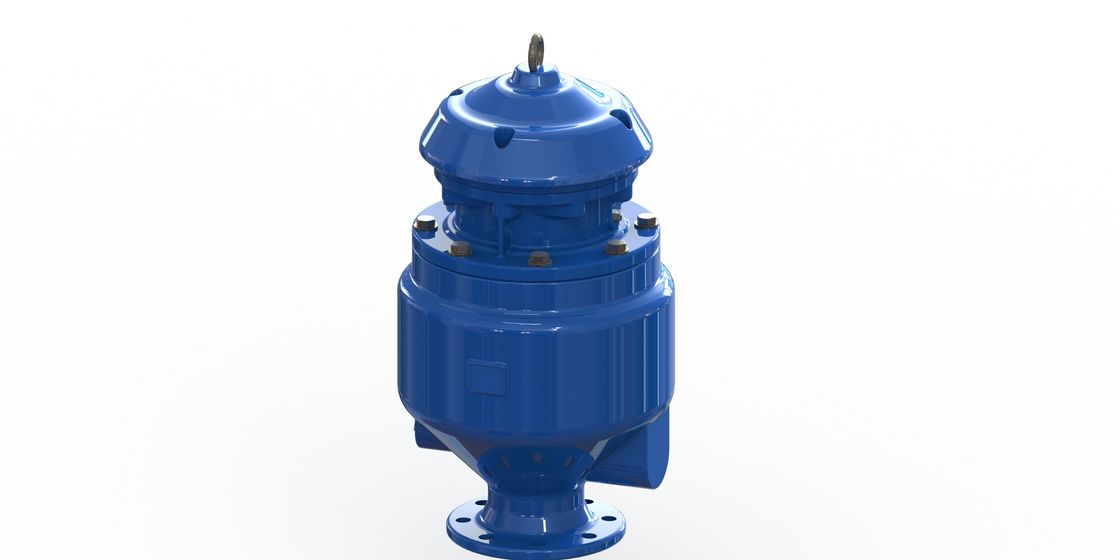
Product Description:
The Sewage Air Release Valve is a critical component designed specifically for efficient and reliable air release in sewage and water supply systems. Engineered with precision, this valve ensures optimal performance under various operating conditions, making it an indispensable part of sewage treatment and water supply infrastructure. Manufactured in compliance with the stringent ISO9001-2015 standards, the Sewage Air Release Valve guarantees superior quality, durability, and consistent performance.
One of the standout features of this Sewage Air Release Valve is its advanced kinetic design. This innovative design approach allows the valve to respond swiftly and accurately to changes in air pressure within pipelines, effectively releasing trapped air and preventing issues such as air pockets, flow disruptions, and pipeline damage. The kinetic design not only enhances the valve’s operational efficiency but also contributes to prolonged system life by minimizing wear and tear caused by air accumulation.
Designed to operate at valve temperatures up to ≤80℃, this valve is suitable for a wide range of sewage and water supply applications. It is constructed using high-quality materials that provide excellent resistance to corrosion, ensuring long-term functionality even in harsh environments. The anti-corrosion property is particularly vital in sewage treatment applications, where exposure to aggressive substances is common. Additionally, the valve boasts high temperature resistance, allowing it to maintain its integrity and performance in elevated temperature conditions commonly encountered in sewage and industrial water systems.
The Sewage Air Release Valve is also engineered to withstand high pressure conditions, with pressure ratings available at PN10, PN16, PN25, and PN40. This wide range of pressure ratings makes the valve versatile and adaptable to various pipeline specifications and operational demands. Whether installed in low-pressure water supply networks or high-pressure sewage pipelines, the valve consistently delivers reliable air release performance, thereby enhancing the overall efficiency and safety of the system.
In sewage treatment applications, the valve plays a crucial role in maintaining the smooth flow of wastewater by eliminating trapped air that can cause flow interruptions and pressure surges. By automatically venting air pockets, the Sewage Air Release Valve helps prevent pipeline blockages, reduces the risk of pipe bursts, and ensures stable hydraulic conditions. Similarly, in water supply systems, the valve contributes to maintaining consistent water flow and pressure by efficiently releasing accumulated air, which can otherwise lead to water hammer effects and damage to pumps and other equipment.
Durability and reliability are at the core of this valve’s design philosophy. Its robust construction and compliance with ISO9001-2015 quality management standards assure users of a product that meets international benchmarks for quality and performance. The valve’s anti-corrosion coating and materials selection further extend its service life, minimizing maintenance requirements and operational downtime.
Installation of the Sewage Air Release Valve is straightforward, and it is compatible with a variety of pipeline configurations used in sewage treatment plants and water supply networks. Its compact size and ergonomic design facilitate easy integration into existing systems without requiring extensive modifications. This makes it an ideal choice for both new installations and retrofit projects aimed at improving system efficiency and reliability.
In summary, the Sewage Air Release Valve is a high-performance solution designed to address the critical need for effective air release in sewage and water supply systems. With its kinetic design, compliance with ISO9001-2015 standards, anti-corrosion properties, high temperature and pressure resistance, this valve stands out as a reliable, efficient, and durable choice for engineers and operators. Its application in sewage treatment and water supply ensures enhanced operational stability, reduced maintenance costs, and prolonged system lifespan, making it an essential component for modern fluid management infrastructure.
Features:
- Product Name: Sewage Air Release Valve
- Valve Connection Type: Flange/Thread
- Valve Application: Sewage Treatment and Water Supply
- Valve Type: Sewage Air Release Valve
- Valve Size Range: DN50-DN200
- Valve Body Material: Durable Ductile Iron
- Coating: Fusion Bonded Epoxy for enhanced corrosion resistance
- Design ensures No Harm Liquid Spilling during operation
- Manufactured according to ISO9001-2015 quality standards
Technical Parameters:
| Valve Type |
Sewage Air Release Valve |
| Valve Pressure |
PN10 / PN16 / PN25 / PN40 |
| Valve Temperature |
≤80℃ |
| Valve Connection Type |
Flange / Thread |
| Valve Feature |
Anti-Corrosion / High Temperature Resistance / High Pressure Resistance |
| Valve Body Material |
Ductile Iron with Fushion Bonded Epoxy Coating |
| Valve Size |
DN50 - DN200 |
| Valve Application |
Sewage Treatment / Water Supply / Sewage Water System |
| Design |
Kinetic Design for Enhanced Performance |
Applications:
The Sewage Air Release Valve, available under the trusted AFC and OEM brands with model numbers SKAR and SKAA, is engineered to meet the demanding needs of modern sewage water systems. Originating from China, this valve is designed with a ductile iron body, ensuring exceptional durability and strength. Its robust construction provides excellent resistance to corrosion, high temperatures, and high pressure, making it ideal for use in various sewage applications where reliability and longevity are paramount.
With valve sizes ranging from DN50 to DN200, the Sewage Air Release Valve offers versatile installation options suitable for different pipeline dimensions. It can withstand valve pressures of PN10, PN16, PN25, and PN40, and can operate efficiently at temperatures up to 80℃. These specifications make it highly adaptable to a wide range of sewage water system requirements, ensuring optimal performance under diverse operating conditions.
One of the primary application occasions for this valve is in municipal and industrial sewage water systems where the automatic release of accumulated air is crucial to maintaining system efficiency and preventing pressure buildup. The valve’s anti-corrosion and high-temperature resistance features enable it to perform reliably in harsh environments where sewage water may contain aggressive chemicals or elevated temperatures.
In scenarios such as wastewater treatment plants, sewer pipelines, and drainage systems, the Sewage Air Release Valve plays a vital role in facilitating smooth fluid flow by preventing air blockages. Its design ensures no harm liquid spilling during operation, thereby protecting the environment and maintaining system integrity. The valve complies with ISO9001-2015 quality standards, guaranteeing that it meets rigorous manufacturing and performance criteria.
This valve is also suitable for use in high-pressure sewage pipelines, where it helps to regulate pressure fluctuations and avoid damage to the infrastructure. Its ductile iron body material provides the necessary strength to withstand mechanical stresses, while its precise engineering ensures reliable sealing and air release functionality. Whether installed in new sewage water systems or as a replacement in existing setups, the AFC and OEM Sewage Air Release Valve is a dependable choice for ensuring safe, efficient, and environmentally friendly operation.


 Your message must be between 20-3,000 characters!